Gouging
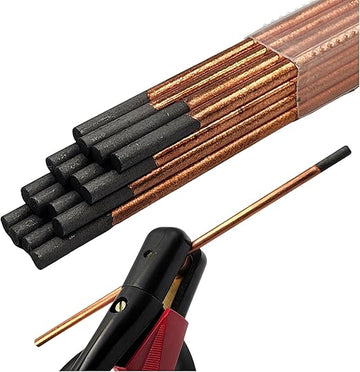
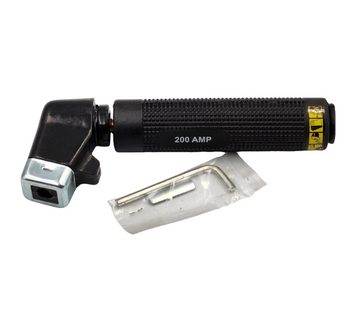
Air carbon-arc gouging torches and pointed and flat gouging carbons for weld removal, back-gouging and metal cleanup.
How air carbon-arc gouging works
An arc between a copper-coated carbon electrode and the work melts the metal, and a jet of compressed air blows the molten metal out of the groove. It removes metal far faster than grinding and works on steel, stainless and cast iron.
Setup basics
- Polarity - run DC electrode positive (DCEP) for most work.
- Air - supply clean, dry compressed air, typically 80 to 100 psi at the torch, with enough volume. Weak air leaves slag and carbon in the groove.
- Machine - gouging draws high current. Match carbon diameter to the machine's output and duty cycle.
Pointed or flat carbons
Pointed (round) carbons cut a U-shaped groove - the standard for back-gouging and removing defects. Flat carbons remove surface metal and weld reinforcement in a wide, shallow pass.
Technique and clean-up
Keep the air jet behind the arc, pointing along the groove. Grind out the carbon-rich surface layer before rewelding, especially on stainless and hardenable steels. Gouging is loud and throws molten metal - wear hearing protection and full FR clothing.
See cutting and gouging and, for plasma gouging, plasma cutting.
Trade and volume pricing: call 905-919-1177 or email orders@mapindpro.com.
Free shipping over $175 across Canada. Counter pickup in North York.