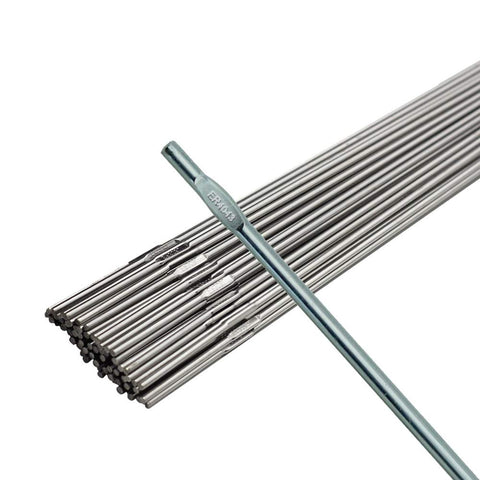
Aluminum TIG Rods
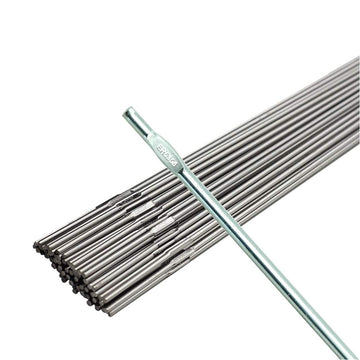
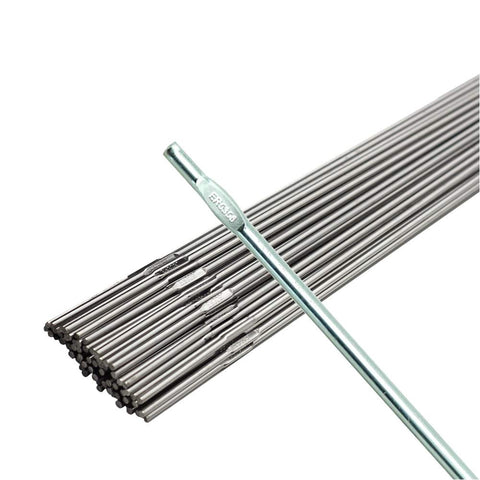
Aluminum TIG filler rod. TIG is the process that gives aluminum the control it needs, and the filler choice follows the base alloy exactly as it does on MIG.
4043 or 5356
- ER4043 - silicon-bearing, flows more easily, lower melting point, better crack resistance on 6061 and other 6000 series alloys. Produces a duller finish and will not anodise to match the base metal.
- ER5356 - magnesium-bearing, higher strength and ductility, anodises close to the base metal. The choice for 5000 series, marine work and anything structural. Also the stiffer rod, which some welders prefer to feed by hand.
Where appearance after anodising matters, that decision alone frequently settles the filler choice.
AC, and balance control
Aluminum TIG runs on AC. The electrode-positive half of the cycle strips the oxide layer; the electrode-negative half puts heat into the work. AC balance control is how you trade cleaning action against penetration - more cleaning for dirty or heavily oxidised material, more penetration once it is clean.
Rod size and heat
Filler rod diameter should be close to the material thickness. Too thin and it melts before it reaches the puddle; too thick and it chills the puddle and stops fusion.
Store rods sealed
Aluminum filler picks up oxide and moisture in open storage, and both end up in the weld as porosity. Keep tubes closed, and wipe rods with acetone before use if they have been out.
Free shipping over $175 across Canada. Counter pickup in North York.