
Steel Welding
Consumables for mild and structural steel, covering stick, MIG and TIG. This is the highest-volume category in the shop and the one where getting the classification right matters most, because steel filler is chosen by the code the job is welded to, not by preference.
Stick electrodes
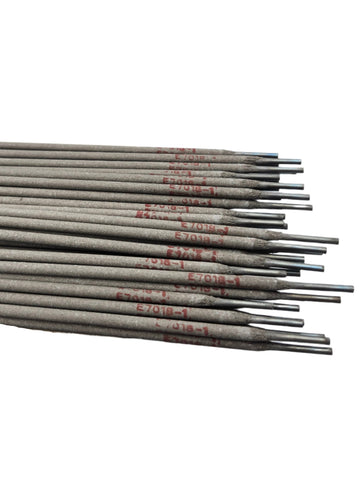
- E6010 - deep penetration, aggressive arc, runs on DC. Root passes, pipe, and dirty or rusted material.
- E6013 - soft arc, easy restart, light penetration. General repair, sheet and light fabrication, and the usual choice for training.
- E7014 - iron powder, high deposition, smooth bead. Fast fill on clean material where appearance matters.
- E7018 - low hydrogen, 70,000 psi tensile. The structural standard. Keep it dry; a low-hydrogen electrode that has absorbed moisture is no longer low hydrogen.
MIG wire
ER70S-6 is the workhorse for mild steel, with enough deoxidiser to tolerate mill scale and light surface contamination. Match diameter to material thickness and to the amperage range of your machine, not to what is already on the shelf.
TIG rods
ER70S-2 and ER70S-6 cover most mild steel TIG work. ER70S-2 carries additional deoxidisers for root runs and less-than-clean material.
Storage is part of the spec
Low-hydrogen electrodes and TIG rods both degrade in open storage. Rod ovens and sealed containers are stocked alongside the consumables for exactly this reason.
Free shipping over $175 across Canada. Counter pickup and bulk pricing available at our North York location.
 Steel Welding
E6013 Steel Stick Electrodes – 1/8" (3.2mm)
$42.99 Steel Welding
ER90S-B3 Steel TIG Welding Rods
$199.00 Steel Welding
ER80S-D2 Steel TIG Welding Rods
$139.00 Steel Welding
E6010 Steel Stick Electrodes – 5/32" (4.0mm)
$39.00 Steel Welding
E6013 Steel Stick Electrodes – 5/32" (4.0mm)
$47.90 Steel Welding
E7014 Steel Stick Electrodes – 3/16" (4.8mm)
$53.10
How to Choose the Right Welding Helmet: Shade Numbers, Safety Standards, and Features
A shade-number-first, CSA/ANSI-grounded buying guide to choosing a welding helmet for MIG, TIG, Stick, and plasma work — fixed vs. auto-darkening, sensors, PAPR, and MapleWeld's lineup...